Containment Solutions for a Leading Battery Recycler
The rapid growth of electric vehicles has accelerated demand for efficient recycling of End of Life batteries. Recovery of materials from EOL batteries presents unique hazards, requiring robust containment to safeguard operators and maintain environmental compliance.
CAS was selected by a leading recycler to design and deliver a suite of custom enclosures that would integrate directly into their pilot lines, supporting large scale recycling operations.

the challenge
Pack off and Weighing Containment
Manual bagging and weighing presented high risk points for powder exposure. The client required engineered enclosures that would provide airflow control and protection for operators while still allowing weighing and smooth handling of material transfers.
Transfer Point Control
Dust presented a significant challenge at transfer points where material moved from loading systems to vibratory feeders and onward through the recycling line. CAS needed to create modular housings, directly coupled to plant equipment upstream and downstream from the process. Addressing critical hazard points required finite design and engineering controls, ensuring the end result contained dust effectively while still giving operators access for maintenance and cleaning.
Working from 3D Models
Unlike many projects where site surveys provide the foundation, this facility was designed in 3D models. CAS had to engineer enclosures that would integrate precisely into the digital reference, taking into account scale, datum points, penetration for extract and anchoring positions (critical for compliance with State building code.) This added complexity to the design but ensured seamless integration once fabricated.
Phased Delivery
The clients programme called for phased installation to match broader project sequencing. CAS needed to design enclosures that could be installed in sections and assembled efficiently, while ensuring performance was not compromised by the modular approach.
Our Solution
Bagging Stations
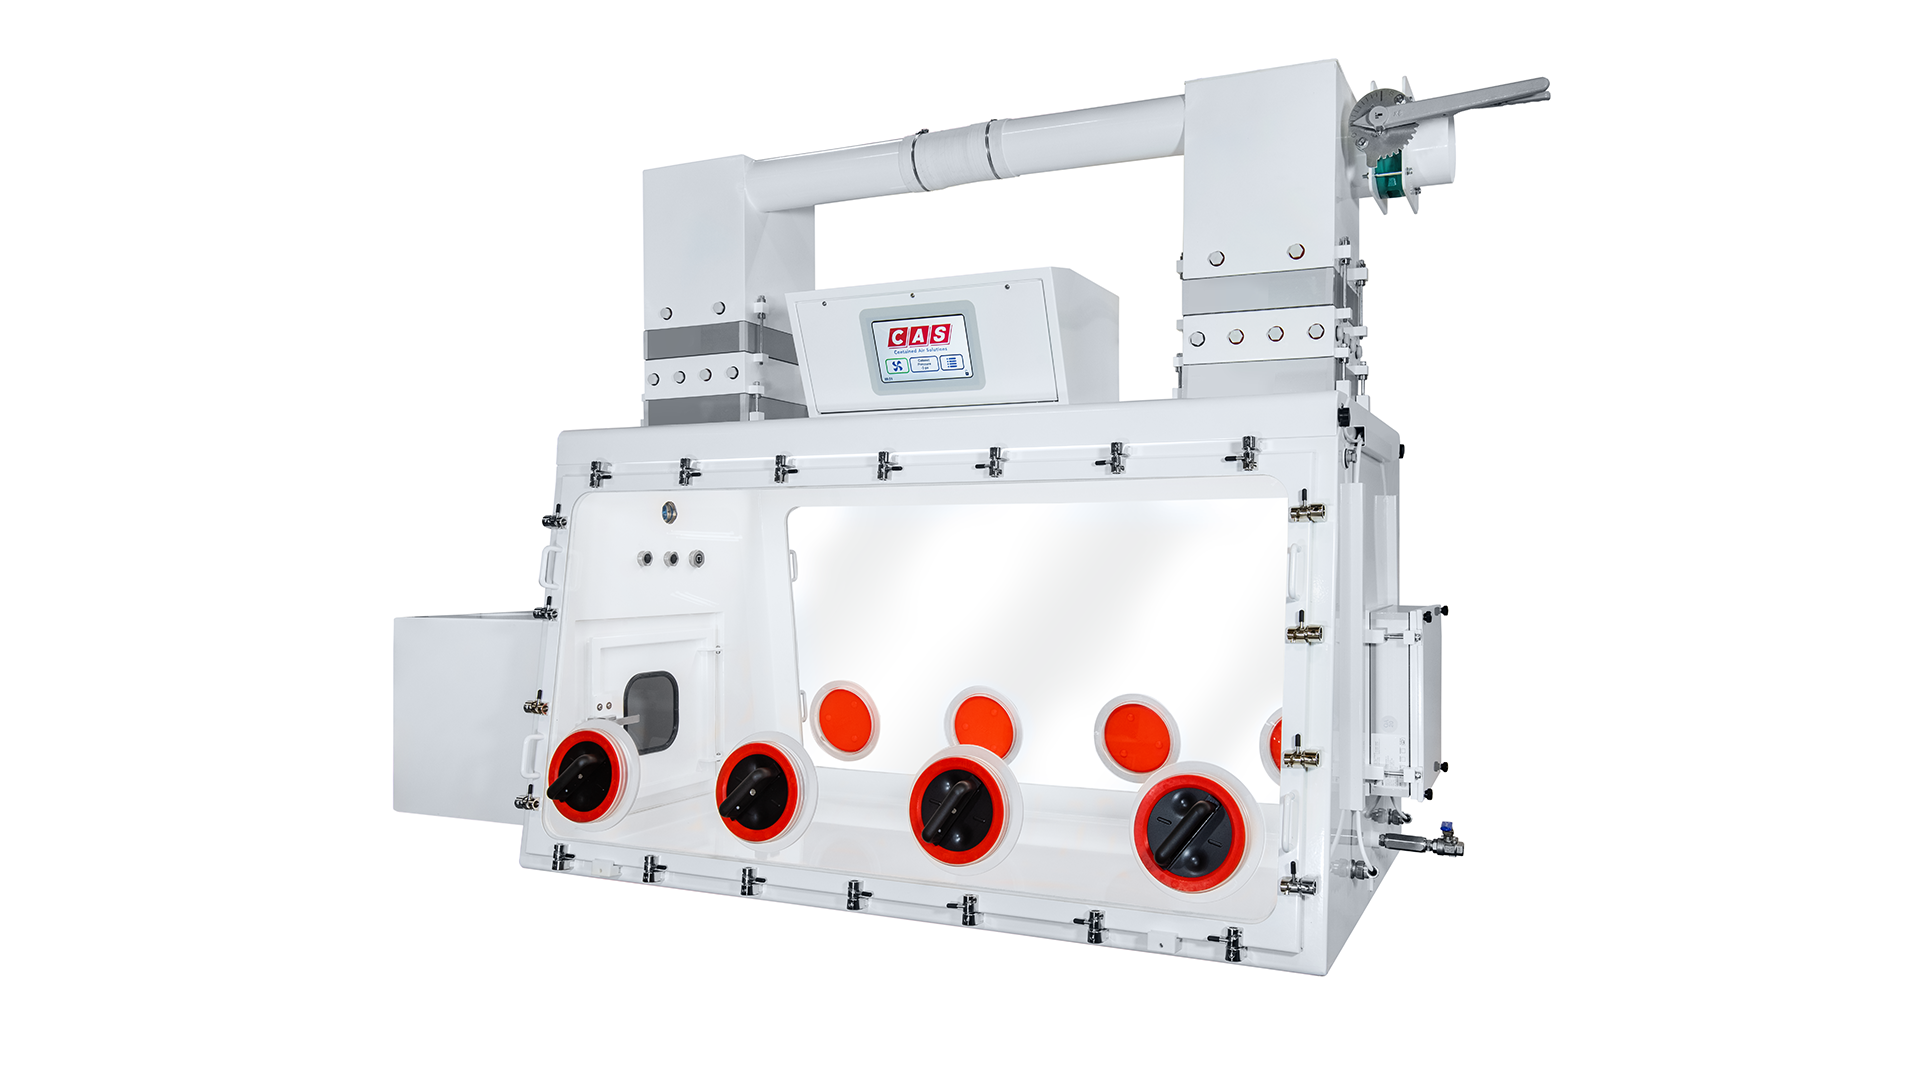
The pack off enclosures were engineered with duct to facility extract and directional airflow to contain powders at the point of discharge. Hinged access doors and removable panels supported safe operator interaction and long term maintenance.
Plastic Weigh Scale Enclosure
Custom enclosures were designed for bulk bag weighing in a controlled environment. These units incorporated reinforced structures, removable side panels, vision panels within roof and side wall frames, material feed transfer points, providing both containment and usability for the operators.
Vibratory Feeder Enclosure
Large modular housing were developed to sit above feeders and conveyors, containing dust at transfer points. Access hatches, flexible flange interfaces and tipper integration were built into the design to maintain operator access while protecting users in the process.

Implementation
Collaboration with the clients engineering, logistics and site team was critical. CAS worked from the full 3D line models to ensure accurate scale, positioning and service integration. Designs were refined through multiple stages to capture evolving requirements and final enclosures were fabricated for phased delivery.
The Result
Engineered Operator Protection
The enclosures were designed to provide operator protection in line with the exposure targets defined by the clients team, using directional airflow and controlled environments to reduce potential exposure
Dust Classification Strategy
Each unit was engineered to connect to facility extract and maintain airflow in accordance with the clients dust control classification. The design intent ensured that ventilation paths were defined and contamination risks addressed.
Contained Weighing and Pack off
By creating low turbulence environments around weighing and discharge operations, CAS enabled controlled handling without disrupting processes or compromising containment.
Maintainability and Access
Removable panels, hinged doors and modular construction ensured the clients team could carry out cleaning, changeovers and long term maintenance without compromising enclosure integrity.


Looking Ahead
This project highlights the value of engineered containment in emerging industries such as battery recycling, while also underlining the relevance to broader markets where hazardous powders are handled. CAS remains focused on developing flexible, modular systems that enable safe, compliant processes across industrial, advanced materials and the life science sectors.